
“The China supply chain” is a phrase that hides the thing it describes. There is no single chain. There are regional clusters, each with its own specialism, its own labour market and its own way of quoting, and an order that crosses two of them behaves differently from an order that sits inside one.
Buyers get hurt by the assumption of uniformity in a specific way: they plan an order as if one supplier, one lead time and one quality standard applied, then discover that the outer component comes from a different province, the assembly from a second, and the packing from a third — each with a separate calendar.
This is written for buyers who already source in China and are trying to work out why a predictable order stopped being predictable, rather than for buyers deciding whether to source there at all.
The instinct, once the problem is understood, is to cut the number of links: fewer suppliers, fewer agents, fewer conversations. That instinct usually fails, because a cross-market order cannot be made simpler by removing participants — the work still has to happen somewhere, and when it happens out of sight it becomes a surprise instead of a task.
What actually changes the outcome is the opposite: making each link visible. Which site, which commitment, which document, which date. An order that crosses four regions is manageable when each stage can be seen and checked; it is unmanageable when it is consolidated into one invoice and one promise, however few names appear on it.
Why the country is organised into clusters rather than into one market
Three forces push production into clusters, and all three are structural rather than temporary.
The first is labour. Specialised skills concentrate: a region that has made a category for twenty years has supervisors who can train new workers quickly, and a region that has not, does not. The second is supply of components. Once enough assemblers sit in one place, component makers move next to them, and the assemblers become dependent on that proximity. The third is the trading layer that grows around both — the packers, the forwarders, the testing labs, the agents who know which factory actually has capacity this month.
The consequence for a buyer is simple and uncomfortable: the cluster is the unit of capability, not the country. A supplier list organised by product category, with no column for location, is a list that will produce surprises.
The three layers an order actually passes through
Most purchase orders are described as one transaction and executed as three.
Component and material. Where the fabric, the board, the motor or the resin comes from. This layer is the least visible to buyers and the most common cause of delay, because it sits upstream of the supplier who quoted.
Assembly and finishing. Where the product becomes the product: cutting, moulding, stitching, printing, packing. This is the layer buyers usually visit, and the one they mistake for the whole.
Consolidation and exit. Where cartons from several assemblers are joined, documented and moved. This layer determines whether a multi-supplier order leaves as one shipment or four.
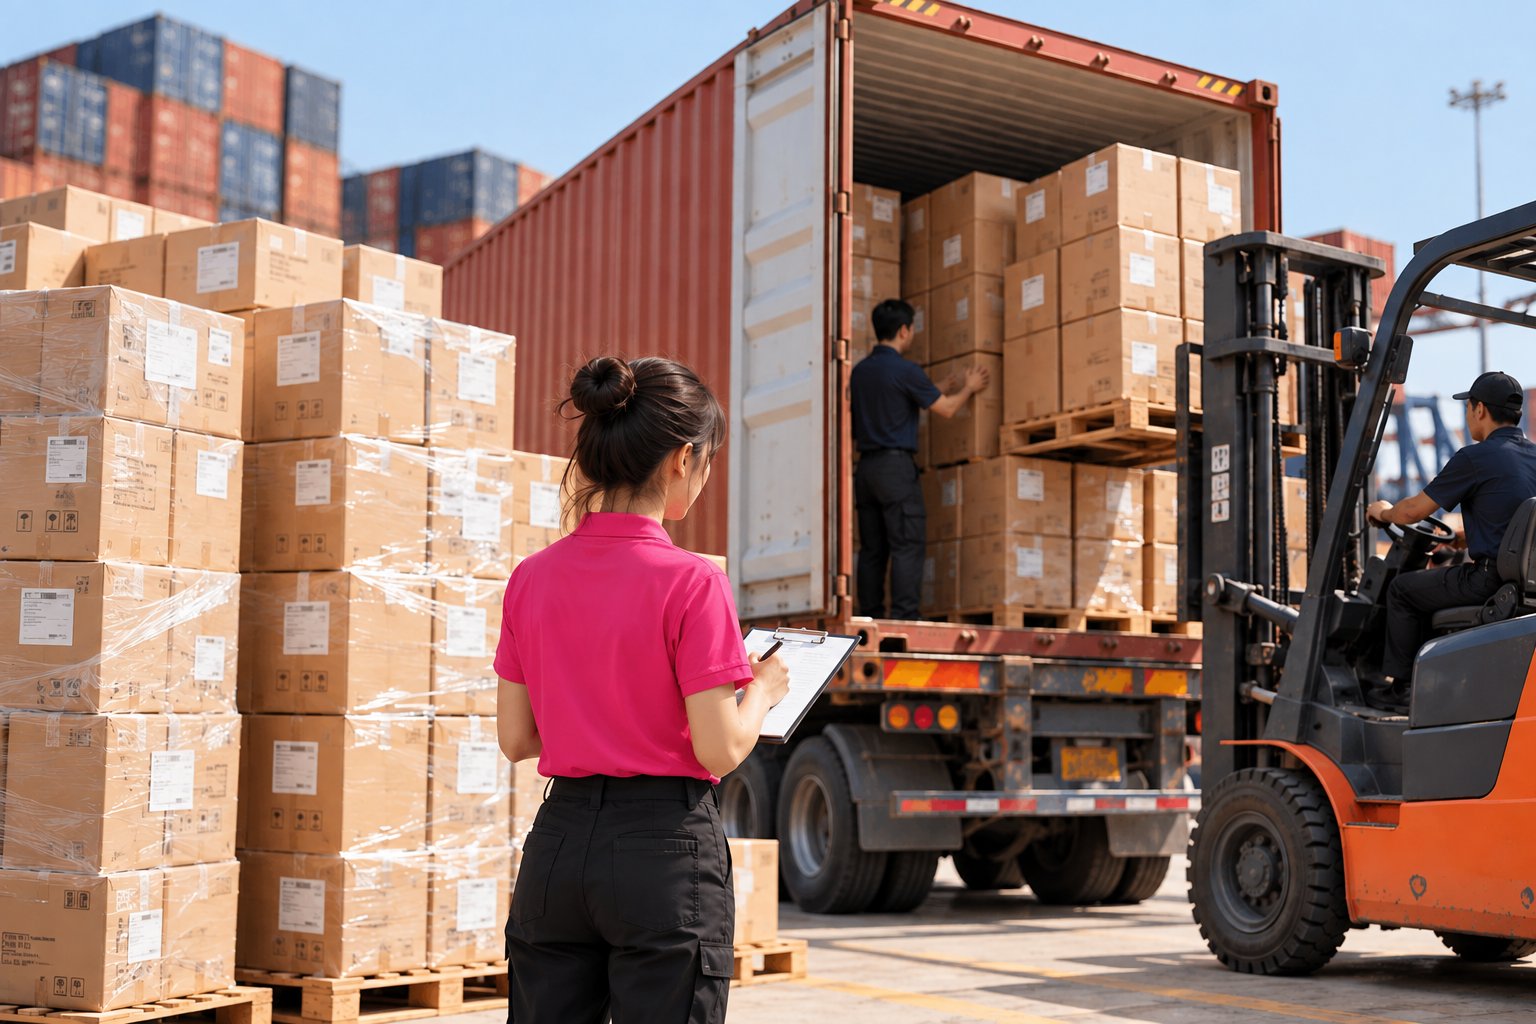
A supply chain problem that appears at layer three is often created at layer one, and diagnosed at layer two. Buyers who only have visibility at layer two spend their time negotiating with the party that has the least control over the cause.
What regional division does to an order structure
Once a buyer accepts that capability is regional, the order structure changes in three ways.
The bill of materials stops being a purchasing document and becomes a map. Each line has a location, and the locations cluster or they do not. A bill where nine of eleven lines sit in one region is a different project from one where the lines are spread across four.
Lead time stops being a number and becomes a sequence. The critical path runs through whichever layer starts last, and that is usually the component layer, not the assembly layer that quoted the delivery date.
Quality stops being a single inspection and becomes a handover problem. Each transfer between clusters — component to assembly, assembly to consolidation — is a point where specification can drift, because the party receiving the goods did not write the specification.
The hidden cost of treating China as a single source
The costs of the uniformity assumption do not appear on a quotation. They appear later, in four places.
Expediting. When a component is late and the assembly slot cannot move, the fix is air freight or overtime, and both are paid by the buyer.
Re-inspection. Goods assembled from components of uneven quality fail inspection at a higher rate, and the failure is attributed to the assembler who had least control.
Inventory drift. Buyers buffer against uncertainty by ordering early, which ties up cash in goods that sit in a warehouse because the rest of the order is not ready.
Management time. The largest and least visible cost. A spread order consumes coordination hours that never appear in a landed-cost calculation, and those hours are the buyer’s own.
None of these are arguments against multi-region sourcing. They are arguments against planning it as if it were single-region.
Where visibility breaks
Coordination between clusters fails at three specific seams, and each has a practical test.
The specification seam. The component supplier works to a drawing; the assembler works to a sample. If the two documents disagree, the disagreement is discovered at assembly. The test: ask both parties to state the tolerance they are working to, and compare the answers.
The scheduling seam. Each party plans against its own capacity, and the date the buyer was given belongs to nobody in particular. The test: ask which party committed to which date, and see whether the answer names stages or only a final figure.
The documentation seam. Cartons, labels and certificates are produced by different parties, and the set that arrives at the port is assembled by nobody in particular. The test: ask for a sample of the full document set for a recent shipment, before placing the order.
Each seam has the same shape: information exists, but it exists on one side of a handover and not the other. Nothing is added by removing a participant from the chain; something is added by recording the same facts on both sides, in a form the next party can check.
Consolidation is not integration
These two are sold with similar language and they produce opposite results.
Consolidation joins shipments. Cartons from four suppliers arrive at one warehouse, are loaded into one container, and leave under one document set. The invoice becomes simpler. The underlying production, quality and timing are unchanged, and the buyer sees a single number where there were four — which is helpful right up to the point where something goes wrong and the single number has no explanation behind it.
Integration makes the chain visible while it is being joined. The same four suppliers, the same container, but each link keeps its own recorded site, committed date, specification version and inspection result, and those records are held together as one file that both sides can read.
The difference shows up at the first exception. Under consolidation, the question “where did this delay start” is answered by reconstructing events after the fact. Under integration, it is answered by reading the record — which is the whole point, because problems are cheaper to fix while they are still small and attributable.
What makes a cross-region order traceable
Four decisions, taken before the order is placed, do most of the work.
Record the production site for every line, not only the supplier name. Fix the specification at each handover in writing, with the receiving party acknowledging the version it received. Hold a schedule that carries each stage’s own committed date, rather than one delivery date for the whole order. And decide the exit before production starts — one consolidation point or several shipments — because that decision determines how inspection has to be scheduled.
The last one is the most often deferred and the most expensive to change. An inspection plan written for one shipment does not work for four, and rewriting it after production has started costs more than planning it before.
None of these are reports. They are records created at the moment the event happens, in a form that survives the person who made them.
Where MU Group sits
MU Group works as a sourcing and supply chain partner rather than a manufacturer, and the role it takes on a cross-market order is the second of the two above: integration rather than consolidation.
That means supplier management, order execution, quality control, warehousing and logistics are handled as one connected process rather than as separate services bought from separate parties. The purpose is not to reduce the number of conversations — a cross-region order will always need many — but to make the chain readable: which site is producing, what was committed at each stage, what was checked and against which standard, what is waiting where.
Three outcomes follow from that, and they are the ones buyers actually feel. Problems surface earlier, because a delay or a specification drift is recorded when it happens rather than discovered at loading. Cooperation between stages improves, because each party can see what the others committed to. And the buyer stops reconstructing events from memory, because the record exists before the question is asked.
The group structure matters here for a geographic reason: the operating centres and branch offices sit in the regions where the clusters are, which is what makes a cross-region order practical rather than theoretical. The branch office network shows where the group operates, and the service scope describes what is done at each stage. Buyers planning an order that spans more than one region can describe the structure first — the structure, not the product, is what determines whether the plan holds.
Frequently asked questions
Is it cheaper to keep the whole order in one region?
Usually, if the region can do all of it. The saving is coordination rather than unit price, and it disappears when the region has to buy a component in from elsewhere anyway.
How many regions is too many?
The limit is not a number of regions but a number of handovers whose facts the buyer can no longer see. Two regions with recorded commitments are easier than one region with four sub-suppliers and no record.
Does working through one partner remove the complexity?
It removes the admin, not the work. What matters is whether the partner keeps each link visible — site, commitment, specification and inspection — or collapses them into a single figure that cannot be explained when something goes wrong.
How do we know which layer is causing a delay?
Ask for the date each layer committed to, not the date the supplier committed to the buyer. If the layers cannot produce separate dates, the delay has no owner.
Can this be fixed mid-order?
Partly. The exit decision and the inspection schedule can be adjusted; the component layer usually cannot, because it is already running.